Developing a metal component from an initial CAD concept to a production-ready part requires more than simply checking its shape. Engineers must evaluate dimensions, structural behavior, thermal performance, assembly compatibility, surface quality, and manufacturability. This makes aluminum prototype manufacturing an important stage in industries where design mistakes can become expensive after production tooling begins.
Among available manufacturing technologies, aluminum prototype machining provides an effective combination of dimensional accuracy, material authenticity, repeatability, and design flexibility. CNC-machined aluminum prototypes can closely reproduce the mechanical characteristics of final production components, allowing engineers to perform meaningful functional tests before committing to high-volume manufacturing.
Understanding Aluminum Prototype Manufacturing
Aluminum prototype manufacturing refers to producing one or a small number of aluminum components for engineering validation, functional testing, market evaluation, assembly verification, or pre-production development.
Unlike visual models made primarily to demonstrate appearance, functional aluminum prototypes are manufactured to represent actual engineering performance.
What Can Engineers Validate?
A properly produced aluminum prototype can help evaluate:
- Dimensional accuracy
- Structural strength
- Component fit
- Assembly clearance
- Thermal management
- Vibration resistance
- Mounting positions
- Thread performance
- Surface finish
- Product ergonomics
Prototype Versus Production Component
A prototype may use a different manufacturing route from the final production part. For example, a future die-cast component may initially be CNC machined from billet aluminum because machining avoids expensive tooling and enables rapid design modifications.
How Aluminum Prototype Machining Works
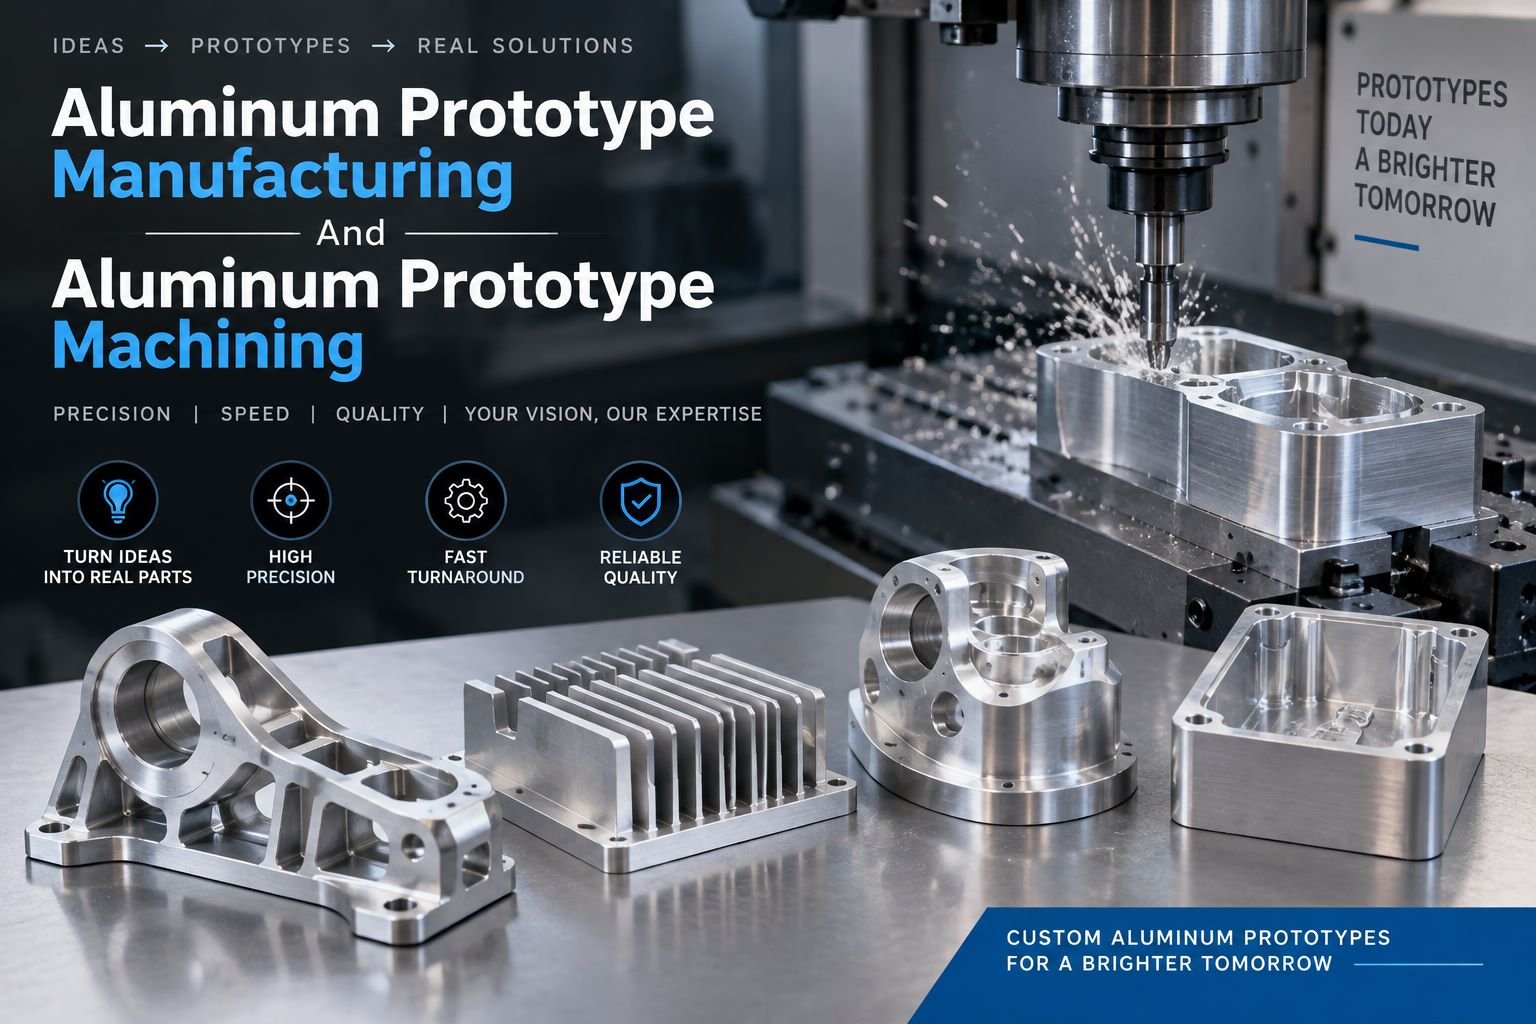
Aluminum prototype machining is primarily a subtractive manufacturing process. Material is progressively removed from aluminum stock until the required geometry is produced.
Modern CNC equipment follows programmed toolpaths generated from 3D CAD data using CAM software.
The general workflow includes:
- CAD model review
- Material selection
- DFM analysis
- CNC programming
- Raw material preparation
- Rough machining
- Precision finishing
- Drilling and threading
- Dimensional inspection
- Surface treatment and final verification
CNC Milling
CNC milling uses rotating cutting tools to remove material from stationary workpieces. It is suitable for pockets, slots, holes, complex surfaces, housings, brackets, and structural components.
CNC Turning
Turning is typically used for cylindrical components. The aluminum workpiece rotates while cutting tools create external diameters, internal bores, grooves, threads, and tapered surfaces.
Multi-Axis Machining
Four-axis and five-axis CNC systems provide additional movement and tool access. They are valuable for complex aluminum prototype machining because fewer setups may be required, improving positional accuracy and reducing manufacturing time.
Aluminum Alloy Selection in Prototype Development
Choosing the correct alloy is critical because aluminum grades differ significantly in strength, hardness, corrosion resistance, machinability, and thermal performance.
| Alloy | Strength | Machinability | Corrosion Resistance | Common Use |
| 6061 | High | Excellent | Excellent | General engineering |
| 7075 | Very high | Excellent | Moderate | Aerospace, structural parts |
| 2024 | High | Good | Moderate | Aircraft components |
| 5052 | Medium | Good | Excellent | Sheet metal products |
Aluminum 6061
6061 is widely used in aluminum prototype manufacturing because it offers balanced mechanical properties, good machining characteristics, weldability, corrosion resistance, and relatively economical material cost.
Aluminum 7075
7075 provides substantially greater strength and is commonly considered when prototypes must withstand high mechanical loads.
Why Material Selection Matters
Using an inappropriate alloy can produce misleading prototype test results. Functional prototypes should therefore use material properties that represent the intended production application as closely as practical.
Critical CNC Machining Design Considerations
A component may look simple in CAD software but become difficult or expensive to machine because cutting tools have physical limitations.
Internal Corner Radius
CNC milling tools are round, meaning perfectly sharp internal corners cannot normally be produced directly. Increasing corner radii allows larger cutters to operate efficiently.
Deep Cavities
Deep pockets require long tools that may experience vibration or deflection. Reducing unnecessary depth can improve accuracy and surface quality.
Thin Walls
Very thin aluminum walls can deform under cutting pressure. Designers should maintain practical wall thickness wherever possible.
Tight Tolerances
Precision tolerances increase manufacturing and inspection requirements.
Rather than applying extremely tight tolerances everywhere, engineers should identify only those dimensions that directly affect function.
Tolerance Strategy
Critical mating surfaces, bearing locations, alignment holes, sealing features, and precision assemblies may justify tighter controls, while non-functional exterior dimensions can often use standard machining tolerances.
Surface Finish and Post-Processing Options
Raw CNC-machined aluminum typically displays visible tool marks. Depending on functional and cosmetic requirements, several secondary treatments can be applied.
Common options include:
- Bead blasting
- Anodizing
- Hard anodizing
- Polishing
- Brushing
- Powder coating
- Painting
- Chemical conversion coating
Anodizing
Anodizing creates a controlled oxide layer on the aluminum surface. It can improve corrosion resistance, wear performance, and appearance.
Bead Blasting
Bead blasting creates a consistent matte texture by impacting the surface with fine media.
Choosing the Right Finish
Surface treatment should be selected according to environmental exposure, appearance requirements, electrical conductivity, dimensional restrictions, and wear conditions.
Quality Control in Aluminum Prototype Manufacturing
Producing a component is only part of the process. Reliable aluminum prototype manufacturing also requires verification that the manufactured geometry matches design requirements.
Typical inspection equipment includes:
- Digital calipers
- Micrometers
- Height gauges
- Thread gauges
- Pin gauges
- Surface roughness testers
- Optical measurement systems
- Coordinate measuring machines
A coordinate measuring machine can verify complex three-dimensional geometry and is particularly useful for high-precision prototypes.
Cost Factors in Aluminum Prototype Machining
The price of aluminum prototype machining depends on more than the amount of aluminum used.
Major cost drivers include:
| Cost Factor | Influence |
| Complex geometry | More machining time |
| Tight tolerances | Additional precision and inspection |
| Multiple setups | Increased labor and alignment |
| Deep pockets | Longer machining cycles |
| Specialty material | Higher raw material cost |
| Surface finishing | Additional processing |
| Small quantity | Setup cost spread over fewer parts |
How to Reduce Prototype Cost
Engineers can reduce unnecessary expense by standardizing hole sizes, increasing internal radii, avoiding excessively tight tolerances, minimizing machining setups, and selecting readily available material grades.
Industries Using Aluminum Prototypes
Aluminum prototypes are widely applied across advanced industries.
Applications include:
- Aerospace structural components
- Automotive brackets and housings
- Robotics frames and joints
- Medical equipment components
- Electronic enclosures
- Heat sinks
- Optical equipment housings
- Industrial automation parts
- Drone components
- Testing fixtures
The combination of light weight and mechanical performance makes aluminum particularly attractive where weight reduction is important.
Frequently Asked Questions
1. What is aluminum prototype manufacturing?
It is the process of producing aluminum components in low quantities for testing, design validation, development, and pre-production assessment.
2. Why use CNC machining for aluminum prototypes?
CNC machining provides high precision, good repeatability, excellent material properties, and the ability to manufacture complex geometries.
3. Which aluminum alloy is best for prototypes?
6061 is widely used for general applications, while 7075 is preferred when significantly higher strength is required.
4. Can CNC prototypes have production-level accuracy?
Yes. Modern CNC equipment can produce highly accurate parts when appropriate machining and inspection processes are used.
5. Can aluminum prototypes include threads?
Yes. Internal and external threads can be machined directly or created using threaded inserts.
6. What affects machining tolerance?
Machine capability, cutting tools, component geometry, material stability, temperature, setup quality, and inspection methods all affect tolerance.
7. Is five-axis machining always necessary?
No. It is mainly beneficial for geometrically complex components requiring access from multiple angles.
8. Can machined aluminum prototypes be anodized?
Yes. Anodizing is one of the most widely used finishing processes for aluminum components.
9. How can machining costs be reduced?
Simplify geometry, use practical tolerances, minimize deep cavities, increase internal radii, and avoid unnecessary secondary operations.
10. What files are required for prototype production?
Manufacturers usually require a 3D CAD model, engineering drawing, material specification, quantity, tolerance information, and surface finish requirements.