Among these processes, Zinc Die Casting has become an important solution for producing complex metal components efficiently. The success of the process also depends heavily on a precisely engineered Die Casting Mold, which determines the final shape, tolerance, surface quality, and repeatability of every component.
From automotive fittings and electronic housings to industrial hardware and consumer products, zinc casting technology supports manufacturers that require high-volume production without sacrificing precision.
What Is Zinc Die Casting?
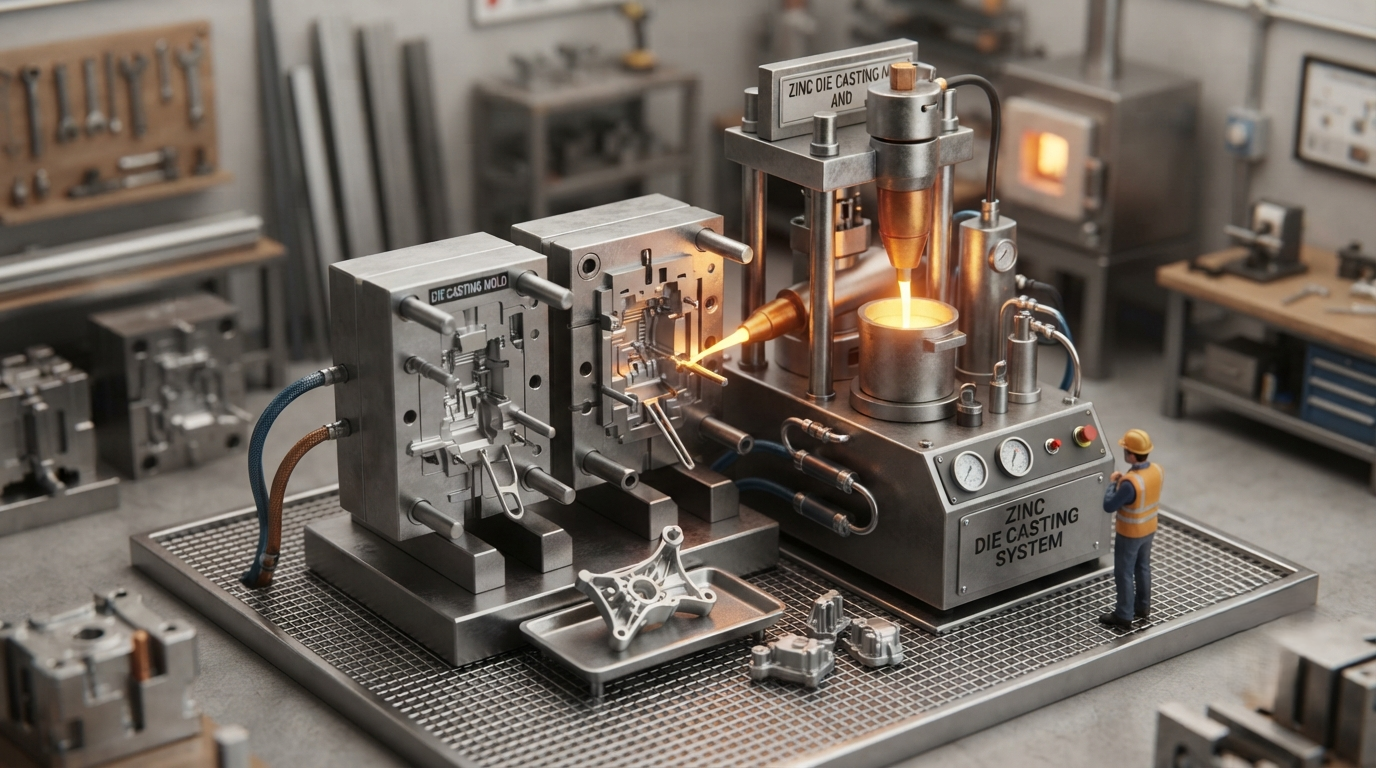
Zinc Die Casting is a manufacturing process in which molten zinc alloy is injected into a hardened steel mold under high pressure. Once the metal fills the mold cavity, it cools and solidifies rapidly. The mold opens, and the finished casting is ejected for trimming, finishing, inspection, or secondary machining.
Zinc alloys are particularly suitable for die casting because of their relatively low melting temperatures, excellent fluidity, strength, and ability to reproduce small design details.
Major advantages include:
- Excellent dimensional stability
- Thin-wall manufacturing capability
- High production speed
- Smooth surface finishes
- Accurate reproduction of complex geometry
- Good mechanical strength
- Long tooling life
- Excellent plating and finishing characteristics
These properties make zinc particularly useful for parts that require both visual quality and functional performance.
Understanding the Die Casting Mold
A Die Casting Mold, often called a die, is the precision tooling into which molten metal is injected. It normally consists of two primary sections: the fixed half and the moving half.
When these sections close together, they create the cavity representing the geometry of the finished component.
A properly designed mold may include:
- Mold cavities
- Cores
- Runner systems
- Gates
- Overflow areas
- Cooling channels
- Venting systems
- Ejector pins
Every feature has an important role. For example, gates control how molten zinc enters the cavity, while vents allow trapped gases to escape during filling.
Poor mold engineering can create defects such as porosity, incomplete filling, dimensional variation, flash, or surface imperfections.
How Zinc Die Casting Works
A typical Zinc Die Casting production cycle follows several carefully controlled stages.
- The mold is cleaned and prepared.
- The two mold halves are securely closed.
- Molten zinc alloy is injected under pressure.
- Metal rapidly fills every cavity and detail.
- The casting cools and solidifies.
- The mold opens automatically.
- Ejector pins release the finished casting.
- Excess runners and flash are removed.
- Components undergo inspection and finishing.
Because each cycle can be completed quickly, the process is highly suitable for medium- and high-volume manufacturing.
Why Zinc Is Ideal for Precision Die Casting
Zinc provides several engineering benefits that distinguish it from many alternative casting materials.
Its excellent fluidity allows molten material to flow through extremely small passages and reproduce detailed mold features. Manufacturers can therefore create complex shapes that would otherwise require several machining operations.
Zinc components can also accommodate:
- Fine lettering
- Logos and branding
- Thin sections
- Internal features
- Detailed textures
- Integrated mounting points
- Threads and inserts
The relatively low casting temperature of zinc can also reduce thermal stress on tooling, contributing to longer Die Casting Mold service life compared with certain higher-temperature alloys.
Zinc Die Casting vs Other Casting Materials
| Feature | Zinc | Aluminum | Magnesium |
| Detail reproduction | Excellent | Very good | Very good |
| Thin-wall capability | Excellent | Good | Excellent |
| Tool life | Very high | Moderate | Good |
| Component weight | Higher | Low | Very low |
| Surface finish | Excellent | Very good | Very good |
| Plating suitability | Excellent | Moderate | Moderate |
| Production speed | Very high | High | High |
The right material depends on product requirements. Zinc is particularly attractive when precision, finish quality, durability, and complex geometry are priorities.
Important Factors in Die Casting Mold Design
The quality of the Die Casting Mold directly affects production efficiency and component reliability.
Engineers should carefully consider several factors before tooling begins.
Part geometry: Sharp corners, deep cavities, and complicated undercuts may increase tooling complexity.
Draft angles: Appropriate draft helps castings release smoothly from the mold.
Wall thickness: Consistent wall thickness encourages uniform filling and solidification.
Gate positioning: Correct gate locations help molten zinc fill the cavity smoothly.
Cooling design: Efficient cooling controls cycle time and dimensional stability.
Venting: Proper venting reduces trapped gas and casting defects.
A well-engineered mold can increase productivity while reducing scrap, rework, and manufacturing costs.
Applications of Zinc Die Casting
The versatility of Zinc Die Casting makes it suitable for numerous industries.
Common applications include:
- Automotive brackets and interior components
- Electrical connectors and housings
- Door and window hardware
- Locks and security components
- Telecommunications equipment
- Medical equipment components
- Industrial machinery parts
- Decorative hardware
- Consumer electronics
- Appliance components
Manufacturers can also apply powder coating, electroplating, painting, polishing, or other surface treatments depending on functional and aesthetic requirements.
Quality Control in Zinc Die Casting
Reliable production requires more than an accurate Die Casting Mold. Process parameters must also remain stable throughout manufacturing.
Professional manufacturers commonly monitor:
- Alloy composition
- Metal temperature
- Injection pressure
- Filling speed
- Mold temperature
- Cooling time
- Dimensional tolerances
- Surface appearance
Inspection may involve dimensional measurement, visual examination, material testing, leak testing, or other procedures based on the component’s intended use.
Consistent quality control helps manufacturers identify process variations before they affect large production quantities.
How to Improve Die Casting Part Quality
Successful die casting begins during product design rather than after production starts.
Manufacturers and designers should work together to optimize component geometry before tooling investment.
Useful practices include:
- Maintain reasonably uniform wall thickness.
- Avoid unnecessary sharp internal corners.
- Provide appropriate draft angles.
- Simplify complicated undercuts when possible.
- Determine critical tolerances early.
- Select appropriate zinc alloys.
- Optimize gate and runner design.
- Plan secondary finishing requirements beforehand.
Early engineering collaboration can significantly reduce tooling modifications and production problems.
Frequently Asked Questions
1. What is Zinc Die Casting?
It is a high-pressure manufacturing process used to produce precise components by injecting molten zinc alloy into steel molds.
2. What is a Die Casting Mold?
A Die Casting Mold is precision steel tooling containing cavities that form molten metal into the required component shape.
3. Why is zinc suitable for die casting?
Zinc offers excellent fluidity, strength, dimensional accuracy, surface finish, and thin-wall casting capability.
4. Is Zinc Die Casting suitable for mass production?
Yes. Rapid production cycles make it especially suitable for medium- and high-volume manufacturing.
5. Can complex components be manufactured?
Yes. Zinc can reproduce intricate features, detailed textures, lettering, and complicated geometries.
6. How long can a Die Casting Mold last?
Tool life depends on mold material, component geometry, maintenance, processing conditions, and production volumes.
7. Can zinc castings receive surface treatments?
Yes. Zinc parts can be plated, painted, polished, powder coated, or treated with other decorative finishes.
8. What causes porosity in die cast parts?
Trapped gases, improper filling conditions, excessive turbulence, and incorrect venting can contribute to porosity.
9. Can thin-wall components be produced?
Yes. Excellent zinc alloy fluidity makes thin and detailed sections possible when parts and molds are engineered correctly.
10. How can casting costs be reduced?
Optimized component geometry, efficient mold design, reduced secondary machining, automation, and larger production quantities can lower unit costs.